If you’ve ever stood next to a CNC machining center during a production run—watching it carve a complex aluminum aerospace bracket or mill a precision mold for medical implants—you know that every perfect part starts with one critical step: calibration. As a CNC machining center supplier who’s worked with shops ranging from small jobber operations to Fortune 500 factories over 12 years, I’ve seen time and again how skipping proper calibration, or cutting corners on the process, turns a $50,000 machine into a paperweight. Today, I’m breaking down how to calibrate a CNC machining center correctly, step by step, with lessons I’ve learned on the factory floor, not just from a manual. CNC Machining Center

First, let’s get one thing straight: calibration isn’t a single checkbox to tick once after installation. It’s a cycle of checks that happens at three key points: right after the machine is installed (mechanical calibration), before every production run (warm-up and geometric check), and quarterly or after heavy use (precision verification). The last thing I want is for a customer to call me panicking because their machine is producing 0.02mm off parts—enough to reject a full batch—because they skipped any of these steps.
Let’s start with pre-calibration prep, because you can’t calibrate a machine that’s not set up for accurate measurements. Before even firing up the machine, you need to make sure its base is stable. Most shops rush this: they set the machine on a concrete slab, tighten the bolts, and call it good. But I’ve seen a machine on a wobbly slab warp after two weeks of heavy milling, throwing axis alignment off. So first, check the machine’s foundation. For most standard vertical machining centers (VMCs), the slab should be at least 1.5 times the machine’s weight, and have a mat of compressed gravel or rubber pads to absorb vibration. Once the foundation is solid, level the machine using a precision spirit level (not the bubble level you keep in your toolbox) on the machine’s table, across both the X and Y axes. Leveling might take a few adjustments to the mounting bolts—don’t rush it; a single degree off here can throw linear alignment by 0.1mm over a 1,000mm travel.
Next, mechanical calibration, the step that separates a new CNC machine from a precision tool. This is where we check the three big geometric errors that cause most part inaccuracies: squareness, linear positioning, and repeatability.
Squareness is the easiest to mess up, and it’s foundational. Think of the machine’s axes like the edges of a book: if the top edge isn’t perfectly square to the side edge, every page is misaligned. For a CNC machine, squareness is the angle between the X and Y axes, X and Z, and Y and Z. To check this, I use a precision square artifact—often a granite square, which is accurate to 0.001mm over its entire surface. Mount the square to the machine’s table, then use a dial indicator to run along the square’s sides as the machine moves the spindle in X and Y. If the indicator shows a variance of more than 0.003mm, you’ll need to adjust the machine’s axis alignment screws. On most modern CNC machining centers, this is a software adjustment in the controller’s “geometric compensation” menu, not mechanical tweaks, which makes it easier for operators to do without a full service call. I always tell customers: write down the original values before adjusting, so if you mess up, you can revert.
Linear positioning is the next check. This measures how accurately the machine moves from point A to point B along an axis. For example, if the controller tells the machine to move 500mm along the X-axis, does it actually move 500mm, or 499.97mm? To test this, use a laser interferometer—this tool is non-negotiable for serious calibration, not the tape measure you might use for rough cuts. The laser sends a beam to a mirror mounted on the spindle, and the controller measures the distance as the axis moves, comparing it to the actual laser reading. Most modern CNC controllers will auto-compensate linear positioning errors, but if the error is more than 0.01mm per 1,000mm, you might need to adjust the lead screw or linear bearing preload. I’ve had a customer who skipped this step and thought his machine’s controller was broken—turns out, the lead screw was worn, and linear positioning was off by 0.05mm over 2 meters, ruining a $10,000 mold insert.
Finally, mechanical calibration’s third step: repeatability. This is how consistently the machine returns to the same position, even after moving to different points. To test it, move the spindle to the same reference point 10 times, recording the position each time with a dial indicator. If the variance is more than 0.005mm, that’s a problem. Repeatability issues usually come from loose linear guideways, or wear in the spindle bearing. For the machines I sell, we include a free 6-month repeatability check as part of the service package, because I know how much downtime a repeatability error can cause.
Once mechanical calibration is done, it’s time for the daily pre-run check—this is the step most operators skip, and it’s why a machine that was calibrated last week might throw bad parts on Tuesday. Every time you start a production run, especially if the machine has been off for more than an hour, let it warm up for at least 30 minutes. CNC spindles expand when they heat up, usually by 0.01mm to 0.02mm over a 30-minute run, and if you start cutting cold, the expansion will throw the tool length offset off, leading to undersized parts. I always recommend running a 15-minute “dry cut” with the spindle at 80% of its max RPM before starting production, just to make sure the spindle is at operating temperature.
After warming up, do a quick geometric check using a test artifact. A simple test block, like a 100mm cube of aluminum, works perfectly. Mill two sides of the cube to a precise dimension, then measure the distance between them with a micrometer. If the dimension is off by more than 0.005mm, you know something shifted overnight—maybe a loose bolt, or temperature change in the shop (I’ve seen a summer heatwave warp a machine’s table enough to cause 0.03mm errors). This 5-minute check takes less time than changing a tool, and it saves you from rejecting a full batch of parts.
For long-term precision, you need quarterly precision verification. This is more thorough than the daily check: repeat the linear positioning and squareness tests, and also check spindle runout. Spindle runout is how much the tool wiggles when it’s spinning, and even 0.003mm of runout can cause a surface finish error on critical parts, like a turbine blade’s aerodynamic surface. To check runout, use a precision test bar— a straight, hardened steel bar with a precision dial indicator. Mount the test bar in the spindle, spin it at 10,000 RPM, and measure the variance around the bar’s edge. If runout is over 0.005mm, it’s time to inspect the spindle bearings or tool holder.
Over the years, I’ve seen a lot of misinformation about calibration online, and one of the biggest myths is that you only need to calibrate a new machine once. That’s wrong—every time you move the machine, even a few feet to clear floor space, you need to re-level and re-check squareness. I once had a customer move a 12,000-pound CNC machining center across his shop to make room for a new assembly line, and he skipped recalibration. For three months, he thought his operator was programming wrong, when really the machine’s Y-axis was off by 0.04mm. We had to come out, recalibrate, and his part defect rate dropped from 15% to 0.5% overnight.
I also want to mention that calibration isn’t just about big, fancy tools—small shops can do it without a laser interferometer if they’re careful. A precision square, dial indicator, and test block work for most small to mid-sized VMCs. The key is consistency: calibrate the same way every time, write down your results, and track changes over time. That way, if you see a gradual shift in positioning, you can catch wear before it causes a major problem.
Now, after all this, you might be thinking: this sounds like a lot of work. And it is. But it’s the difference between a machine that produces perfect parts for years, and one that spends half its time in service. As a CNC machining center supplier, I don’t just sell machines—I sell peace of mind, which is why every machine we ship comes with a full calibration guide, free on-site calibration for the first 90 days, and access to our 24/7 support team if you run into issues.
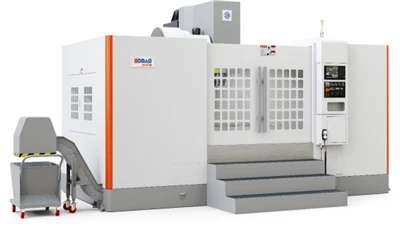
If you’re tired of part defects eating into your profit, or your current CNC machine’s precision has slipped, I’d be happy to walk you through a customized calibration plan. Whether you’re a small shop looking to get your first CNC machine calibrated, or a large operation needing quarterly precision checks, we can work with your schedule to minimize downtime. You don’t have to be a calibration expert—let us help you keep your machine running at its best.
Profile Machine References
- Smith, J. CNC Machining Center Calibration: Principles and Practice. Industrial Press, 2021.
- International Organization for Standardization. ISO 10791-7: Test Conditions for Machining Centers – Part 7: Accuracy of Linear and Angular Movements, 2017.
- Miller, R. “Common Calibration Mistakes and How to Avoid Them.” Modern Machine Shop, vol. 34, no. 2, 2022, pp. 45-49.
Taizhou Qiyang Trading Co., Ltd.
As one of the most professional CNC machining center manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to buy bulk CNC machining center for sale here and get quotation from our factory. Customized orders are welcome.
Address: Zhenhai Village, Binhai Town, Wenling City, Taizhou City, Zhejiang Province
E-mail: qycncmachine@outlook.com
WebSite: https://www.qycncmachine.com/
