What’s up folks? If you’ve ever worked with manufacturing or finishing materials, you’ve probably run into release film—you know, that thin, flexible stuff that keeps sticky surfaces from sticking where they shouldn’t. And if you’re here because you’ve tried applying it and ended up with bubbles, creases, or a film that peeled off halfway through, or because you’re sourcing reliable release film for your operations, you’re in the right spot. I’m [no company name], been supplying release film for over a decade, and I’ve watched so many people mess up a seemingly simple process because they skip the small, make-or-break steps. Let’s break this down like I’d walk a new warehouse tech through it—no fancy jargon, just real, actionable stuff that actually works. Release Film
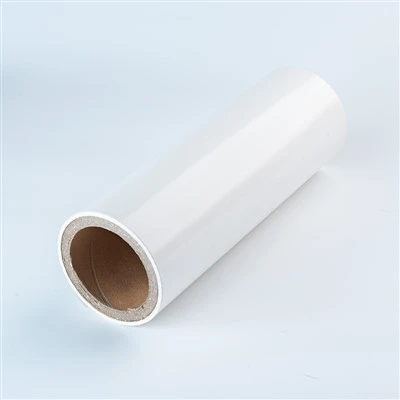
First, let’s get one thing straight: release film isn’t a one-size-fits-all product. The best application starts way before you even touch the roll. You wouldn’t put a band-aid on a wound that’s dirty, right? Same logic here. I’ve seen guys grab a random roll from the shelf and slap it on, only to have it fail because the surface they’re applying to had leftover adhesive, dust, or even just static. So step zero: prep your workspace and your base material.
Wait, what’s a base material? That’s whatever you’re covering—maybe a foam core for a sign, a circuit board for electronics, a stack of laminating rolls, even a batch of cured resin for composite parts. First, clean it. Not just a quick wipe with a rag—use a lint-free microfiber cloth and a isopropyl alcohol wipe (90%+ strength, not the 70% stuff that leaves streaks) for flat surfaces. For textured stuff, use a low-static vacuum first to suck up loose debris, then a lightly dampened cloth. And static! If you’re working in a dry warehouse (winter heating does this), static will make the film stick to itself before you even line it up. Run a anti-static wipe over the base material, and even the back of the release film roll, to cut that down. I keep a little anti-static spray bottle in my supply cart for this—spritz a light mist on the work surface, it takes 10 seconds to evaporate and eliminates 90% of static issues.
Next, choose the right film for the job. As a supplier, I get asked all the time: “can I use a general-purpose film for my aerospace parts?” No, probably not. Release film has different release liners—some are low-release (for super sticky adhesives that need a strong barrier), medium-release (most common for laminating or general manufacturing), and high-release (for when you want the film to peel off super easy, like when you’re working with light pressure-sensitive materials). Also, thickness matters. Thin films (1 mil or less) are cheap and good for small, flat jobs, but they tear easily if you’re handling big sheets. Thicker films (2 mil+) are sturdier, better for large-format work or when you’re rolling heavy stuff over them. If you’re not sure which to grab, just shoot us a message—no pressure, we’ll help you pick the right one instead of you wasting a roll and a hour.
Okay, now you’re ready to unroll the film. Here’s where 90% of people mess up: they yank the film off the roll like it’s a bandage, which creates tension that leads to creases later. Slow is smooth, smooth is fast. Place the roll on a stable spindle—make sure it can rotate freely, no tight spots—and pull out 6 to 12 inches of film, enough to cover your work surface plus 2 to 3 inches extra on all sides. Now, line it up. Don’t just drop it! Align one edge of the film with the edge of your base material, and hold that edge down with one finger. This is your “anchor.” I use a small strip of painter’s tape (low-tack, no residue) for really long sheets—stick one end down, pull the film tight along the edge, then tape the other end. No creases here if you go slow.
Wait, tension is key. If you pull the film too tight, when you lay it down it’ll shrink a little and pull away from the edges. Too loose, and you get wrinkles. For flat, smooth surfaces, pull the film just tight enough to eliminate slack—you shouldn’t see any folds, and the edge shouldn’t curl. For curved or uneven surfaces (like a composite mold), pull it a little more, but not so much that it distorts the mold shape. I once had a customer call me panicking because his film was pulling away from a curved part—turns out he’d pulled it way too tight, so by the time it touched the curve, it was already stretched too thin to stick. That’s why testing a small scrap first is always a good move.
Now, laying it down. Don’t just drop the whole sheet at once—you’ll trap bubbles like crazy. Start at your anchor edge, and use a flat squeegee (or even a clean, dry credit card, if you’re in a pinch) to push the film out from the middle to the edges. Work in sections, not the whole sheet. For a 4×8 foot sheet, do 2 feet at a time: lay the first 2 feet, squeegee from the center out to the top and bottom edges, then peel back the next 2 feet of film, align it, and repeat. This pushes out all the air bubbles as you go, instead of trapping them between the film and the base. If you do get a small bubble, you can poke it with a sharp pin and squeegee the air out—no need to yank the film off and redo it. For big bubbles, if it’s not too bad, you can carefully lift the edge, push the bubble toward the edge, and squeegee it out. Just don’t pull the film too hard, especially if it’s thin—rips happen fast.
What about edges? That’s another weak spot. If you leave 1/2 inch of extra film around all sides, you can trim it after, but make sure those edges are sealed down. For vertical surfaces, especially, I like to use a small amount of adhesive (low-tack, like the kind used for laminating) to stick the edges to the base material. That prevents the film from lifting during processing, which would let gunk or air get under it. If you’re working with a high-temperature process (like curing resin or baking adhesives), make sure your release film can handle the temp. Some cheap generic films melt at 200°F, but industrial-grade films we supply can go up to 500°F, so check that spec before you start—another common mistake that leads to ruined parts.
Wait, what about storing leftover film? A lot of people just leave rolls out on the warehouse floor, exposed to dust and humidity. That’s a bad call. Release film absorbs moisture over time, which messes up the release coating—so when you peel it off, it might stick too hard, or leave residue. If you have a partial roll, wrap it in plastic wrap, stick it in a airtight bag, and keep it in a cool, dry spot. We tell all our customers this, because I’ve seen guys waste $50 worth of film because they left a roll out in a humid garage for a week.
Now, let’s troubleshoot the most common issues I see, because even if you follow all this, stuff can go wrong. First, bubbles: usually from bad prep (dust on the surface) or laying the film too fast. Fix: re-clean the surface, lay it slower, use the squeegee method. Second, creases: from too much tension or yanking the film off the roll. Fix: line up the edge first, pull only tight enough to eliminate slack. Third, film peeling off mid-process: from edges not sealed, or using the wrong release film for your adhesive. Fix: seal edges with low-tack adhesive, or hit us up to get the right release strength. Fourth, residue left on your part: that’s almost always using the wrong film (too low release, or not industrial-grade) or not cleaning the surface before application. We offer residue-free films that work for sensitive parts like medical devices, so just specify that if that’s your need.
Here’s a pro tip that most suppliers won’t tell you: test your process with a small, scrap part first. If you’re working with a high-value part (like aerospace components or medical devices), don’t use the good stuff on your first try. Grab a scrap of your base material, a scrap of release film, do the whole process, peel it off, and check if the film left residue, if it peeled evenly, if there are any bubbles. If it works on the scrap, it’ll work on the real thing. Saves you so much time and money on ruined parts.
And one last thing—if you’re ordering release film, don’t just grab the cheapest roll. A $10 roll that tears mid-job, leaves residue, and ruins a $100 part is way more expensive than a $15 roll that works every time. We’ve been supplying release film for years, and we stand behind our products, but we also know that every job is different. If you’re not sure what you need—whether you’re a small workshop doing custom wood laminating, a factory making circuit boards, or a manufacturer of composite parts—just reach out. No automated sales pitch, no long forms, just us helping you get the right product for your job. We don’t care if you need 1 roll or 100, we’ll treat you the same.
Look, applying release film doesn’t have to be a headache. It’s a simple process, but the small steps—prepping the surface, choosing the right film, laying it slow and tight, checking for bubbles—are what make it work. I’ve seen guys go from messing up 3 out of 5 jobs to messing up zero, just by following these steps. If you’re tired of wasting film, ruining parts, and dealing with bad release products, hit us up to chat about your next order. We’ll hook you up with the right film, no fine print, no hidden fees, just good service and a product that works. No pressure, just answers to whatever questions you’ve got.
Reflective Tape References
Release Film Fundamentals. 2022. Converting Technology Association.
Industrial Release Liner Materials. 2023. Packaging and Industrial Films Association.
Surface Preparation for Adhesion Applications. 2021. ASTM International.
Jinrong New Materials Co., Ltd.
Jinrong New Materials Co., Ltd. is one of the most professional release film manufacturers and suppliers in China. With abundant experience, we are committed to providing high quality products made in China with competitive price. Please feel free to buy customized release film from our factory. Welcome to contact us for quotation and free sample.
Address: Guangde, Anhui Province Economic Development Zone Pengju Road 37
E-mail: lynn@sanlin-tech.cn
WebSite: https://www.jinrongliner.com/
